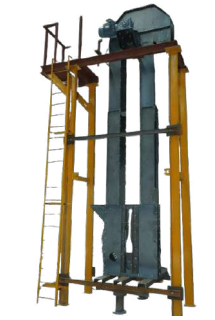
Bucket elevators are commonly used in various industries, including chemicals, minerals, food processing, wood products, and wastewater treatment, to transport free-flowing bulk solids to higher elevations.
These elevators use buckets attached to a belt or chain to move materials. At the elevator’s bottom section, each bucket fills with material as it passes through the inlet, and then it travels upwards to discharge the material at the top section.
These elevators are particularly efficient at transporting material vertically, which is a challenge for many other mechanical conveyors.
Model No
Capacity (m3/hr)
Bucket Size (mm)
Bucket Spacing (mm)
Head Pulley Diameter (mm)
COBE-150
7-12
150 x 150
20-30
400-500
COBE-200
18-27
200 x 200
25-35
400-500
COBE-250
25-48
250 x 310
30-40
600-750
COBE-300
40-70
300 x 300
35-40
600-750
COBE-350
45-75
350 x 300
35-40
600-750
COBE-400
55-90
400 x 300
40
600-750
COBE-450
65-100
450 x 450
40-50
750-1000
COBE-500
90-160
500 x 450
45-50
750-1000
COBE-600
105-200
600 x 450
45-50
800-1000
Features :-
Vertical transport of fine bulk material
Monitoring Belt misalignment
Conveying capacity upto 200 TPH
Conveying heights up to 50 m
Corrosion resistant – completely or partly in stainless steel
Stainless Steel seamless buckets provided for food-grade applications